
 Products
 Martindale abrasion tester Updated
 VeriVide Original D65 Tube Light

0%

Fastness Rotary Friction Tester
$0.00
Fastness Rotary Friction Tester

Fastness Rotary Friction Tester
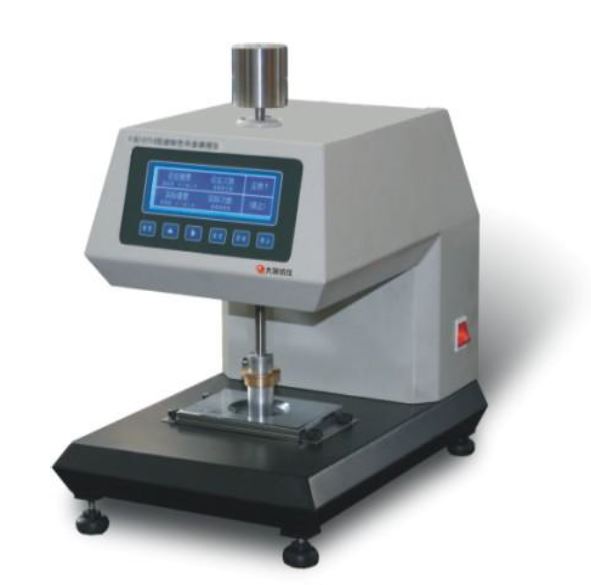
A Fastness Rotary Friction Tester, also known as a Rotary Crock meter, is a specialized instrument used to evaluate the color fastness of textiles and materials when subjected to rotational rubbing. This test simulates the wear and friction that fabrics experience during use, helping manufacturers assess the durability of dyes and finishes.
Purpose of Fastness Rotary Friction Tester
The primary function of the Fastness Rotary Friction Tester is to determine how well a fabric’s color withstands rubbing, both in dry and wet conditions. This is crucial for ensuring the longevity and appearance of textiles in real-world applications, such as clothing, upholstery, and footwear.
Working Principle of Fastness Rotary Friction Tester
The tester operates by applying a specified pressure to a fabric sample using a standardized rubbing finger covered with a test cloth. The rubbing finger performs a set number of rotational movements (typically 1.125 turns clockwise followed by 1.125 turns counterclockwise) over the fabric surface. After the test, the degree of color transfer to the test cloth and any changes in the fabric’s appearance are evaluated against standardized gray scales.
Common Testing Standards
– AATCC 116: Colorfastness to Crocking: Rotary Vertical Crock meter Method.
ISO 105 X16: Textiles—Tests for color fastness—Part X16: Color fastness to rubbing—small areas.
– SATRA TM8: Color fastness to rubbing.
Key Specifications of Fastness Rotary Friction Tester
– Rubbing Head Diameter: Typically 16 mm.
– Applied Pressure: Approximately 1134 grams (11.1 N).
– Rotation: 1.125 turns clockwise followed by 1.125 turns counterclockwise.
– Sample Size: Commonly 60 mm × 60 mm.
– Test Cloth: Standardized white cotton cloth, either dry or wetted depending on the test condition.
Benefits of Fastness Rotary Friction Tester
– Realistic Simulation: Mimics the actual wear and friction fabrics undergo during use.
– Versatility: Applicable to a wide range of materials, including textiles, leather, and printed fabrics.
– Quality Assurance: Ensures products meet industry standards for color durability.
– Standard Compliance: Aligns with international testing standards, facilitating global trade and quality benchmarks.
Applications Fastness Rotary Friction Tester
– Textile Industry: Assessing the color durability of garments, upholstery, and other fabric products.
– Footwear Manufacturing: Testing the colorfastness of shoe uppers and linings.
– Automotive Interiors: Evaluating the wear resistance of seat covers and other interior fabrics.
Quality Control Laboratories: Routine testing to ensure product consistency and compliance with standards.
Benefits of Fastness Rotary Friction Tester:
- Accurate Colorfastness Evaluation- Provides precise assessment of how well fabric resists color loss and staining from rubbing.
- Simulates Real-World Wear – Recreates rotational friction found in actual use (e.g., seat covers, apparel wear points).
- Supports Wet & Dry Testing – Can test under both dry and wet conditions for comprehensive results.
- Standardized Testing – Complies with global standards (AATCC 116, ISO 105 X16), ensuring reliable and comparable results.
- Time-Saving & Efficient – Quick to set up and run, allowing for high-throughput testing in labs.
- Versatile Use- Suitable for textiles, leather, coated fabrics, and printed surfaces.
- Improves Quality Control – Identifies potential durability issues early in the production process.
- Enhances Product Performance – Helps in developing fabrics with better resistance to rubbing and abrasion.
Features of Fastness Rotary Friction Tester:
- Rotary Rubbing Mechanism – Simulates 1.125 clockwise and 1.125 counterclockwise turns for realistic friction.
- Standardized Rubbing Head – Fixed diameter (typically 16 mm) with specified pressure (≈1134 g) for consistent results.
- Dry and Wet Testing Capability – Can perform tests using dry or wet rubbing cloths.
- Sample Holder- Secure and easy-to-use fixture for holding fabric samples in place.
- Test Cloth Mounting Arm- Quick attachment for standardized white rubbing cloths.
- Simple Operation – Manual or motorized operation depending on model; easy to handle for lab technicians.
- Compliance with Standards – Follows AATCC 116, ISO 105 X16, and SATRA TM8 protocols.
How to Use Fastness Rotary Friction Tester:
- Prepare the Sample – Cut a fabric piece (typically 60 × 60 mm) and condition it per standard requirements.
- Mount the Fabric – Secure the fabric sample on the sample holder or base plate of the tester.
- Attach Rubbing Cloth – Place a standard white test cloth (dry or wetted as required) over the rubbing head.
- Apply Pressure – Lower the rubbing head onto the fabric. Standard weight is about 1134 g.
- Start the Test – Operate the tester: the head performs 1.125 turns clockwise, then 1.125 turns counterclockwise.- Number of cycles (typically 10 or 20) is set based on the test standard.
- Remove and Inspect – After testing, remove the rubbing cloth and assess any color transfer using a gray scale.
- Evaluate Fabric Surface – Check the fabric for visible changes, fading, or wear.
- Record Results – Grade both staining and fabric change per standard gray scale ratings.
Fastness rotary friction tester
[Scope of application]
 It is used to change the color fastness of the textile,
printing and dyeing, printing and other products after a specific track friction.
[Related standards]
GB / T29865 AATCC116 ISO105-X16, etc.
[Instrument characteristics]:
1.Single-chip control, speed can be set freely
2.Imported motor, linear guide, low noise, suitable for long time work
3. Liquid crystal display, film panel
4. Freely set the number of friction, can count up and down,
and automatically stop the alarm when the set value is reached
[Technical Parameters]:
1. Friction head diameter: 16mm 25mm
2. Vertical pressure: 11.1N
3. Working mode: 405 ° clockwise and 405 ° counterclockwise
4. Speed range: constant 60 rpm, LCD display, thin mold panel
5. Counting range: 0-99999 times
6. Power supply: AC 220V 50Hz 80W
7. Weight: 20KG
8. Volume: L420mm × W260mm × H430mm
Shipping & Delivery
Related products
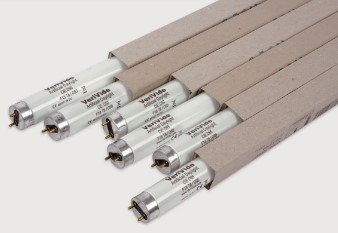

VeriVide Original D65 Tube light
Physical Testing & Fabric Testing, Dyeing Lab Machine, Lab Equipment & Instrument, Yarn Dyeing Machine & Equipment
VeriVide Original D65 Tube Light – Artificial Daylight
VeriVide Original D65 Artificial Daylight Tube Light – 6500K, CRI 98
Original VeriVide D65 Artificial Daylight Tube Light for Accurate Colour Assessment
VeriVide Original D65 Tube Light – Artificial Daylight is a professional standardized daylight light source designed for accurate and consistent visual colour assessment. With a correlated colour temperature of 6500K and high CRI 98, the VeriVide D65 provides a controlled artificial daylight environment for evaluating colours, shades, textiles, garments, printed materials, plastics, paints, packaging and other products where colour consistency is critical.
Natural daylight changes according to the time of day, weather, season, geographical location and surrounding conditions. These changes can create differences in visual colour evaluation. A standardized D65 artificial daylight source provides a controlled lighting condition so that colour decisions can be made consistently. VeriVide explains that using the same standardized artificial light source throughout the supply chain helps reduce problems caused by variations in natural daylight.
The VeriVide Original D65 Artificial Daylight Tube is therefore an important replacement or lighting component for professional colour assessment cabinets, viewing systems and suitable standardized visual inspection environments.
Product Overview
| Specification | Details |
|---|---|
| Product Name | VeriVide D65 Artificial Daylight Tube Light |
| Brand | VeriVide |
| Light Source | D65 Artificial Daylight |
| Correlated Colour Temperature | 6500K |
| Colour Rendering Index | CRI 98 |
| Lamp Type | T8 |
| Available Length | 600 mm / 1200 mm / 1500 mm |
| Available Power | 18W / 36W / 58W |
| Application | Colour Assessment & Visual Inspection |
| Colour Evaluation | Standardized Artificial Daylight |
| Typical Use | Textile, Garments, Printing, Packaging, Paint, Plastic & Manufacturing |
| Manufacturer | VeriVide |
| Product Codes | 600D65 / 1200D65 / 1500D65 |
Specifications are based on VeriVide's published lamp information. Availability of individual lengths/models should be confirmed at the time of order.
What is VeriVide D65 Artificial Daylight?
VeriVide Original D65 Tube light is a standardized daylight illuminant representing daylight with a correlated colour temperature of approximately 6500 Kelvin. VeriVide describes D65 as the international standard measure of daylight based around a mean colour temperature of 6500K.
The purpose of D65 lighting is not simply to provide a bright white light. Instead, it provides a standardized spectral lighting condition suitable for professional visual colour assessment.
Two products can sometimes appear to have the same colour under one light source but look different under another. This phenomenon is known as metamerism. For this reason, professional colour assessment requires controlled and standardized illumination. VeriVide specifically highlights the importance of viewing colour samples under standardized lighting conditions to identify colour differences and metameric effects.
VeriVide Original D65 Tube light is engineered for this type of controlled colour assessment environment.
Why Choose Original VeriVide D65 Tube Light?
Colour evaluation is an important part of quality control in many industries. A small difference in colour can result in rejection of fabric, garments, packaging, printed materials or finished products.
Using ordinary room lighting or an uncontrolled daylight source may produce inconsistent visual results. The VeriVide D65 provides a standardized artificial daylight source designed specifically for professional colour assessment.
Key advantages include:
- 6500K standardized D65 daylight
- High CRI 98
- Designed for accurate visual colour assessment
- Consistent lighting conditions
- Suitable for professional colour matching
- Helps reduce variations caused by natural daylight
- Suitable for colour assessment equipment and viewing systems
- Available in multiple tube lengths
- Suitable for textile and garment quality control
- Useful for identifying colour differences and metamerism
- Original VeriVide replacement lamp
VeriVide states that its D65 lamp has a CRI of 98, allowing colours to be rendered more accurately than lower-CRI light sources.
Technical Specifications
1. Correlated Colour Temperature – 6500K
VeriVide Original D65 Tube light has a 6500K correlated colour temperature.
6500K is the defining colour-temperature characteristic of D65 artificial daylight. It produces a cool daylight appearance suitable for professional colour evaluation.
This is particularly important when colour standards and product samples need to be compared under controlled lighting conditions.
2. High Colour Rendering Index – CRI 98
VeriVide Original D65 Tube light is specified with a CRI of 98.
CRI, or Colour Rendering Index, indicates how accurately a light source renders colours in comparison with a reference light source. A higher CRI is generally desirable for visual colour assessment because it allows colours to be represented more accurately.
For applications such as textile shade matching, garment inspection and product colour comparison, high colour rendering performance is an important consideration. VeriVide lists its D65 lamp with CRI 98.
3. T8 Tube Design
The VeriVide D65 fluorescent lamp is available in T8 format.
The T8 designation refers to the tube diameter/type used by the lamp. The official VeriVide specification lists D65 versions in 600 mm, 1200 mm and 1500 mm lengths, with corresponding 18W, 36W and 58W power ratings.
Available VeriVide D65 Models
VeriVide 600D65
- Length: 600 mm
- Power: 18W
- Tube Type: T8
- CCT: 6500K
- CRI: 98
- Product Code: 600D65
VeriVide 1200D65
- Length: 1200 mm
- Power: 36W
- Tube Type: T8
- CCT: 6500K
- CRI: 98
- Product Code: 1200D65
VeriVide 1500D65
- Length: 1500 mm
- Power: 58W
- Tube Type: T8
- CCT: 6500K
- CRI: 98
- Product Code: 1500D65
These three D65 configurations are listed in VeriVide's official lamp specification.
Application of VeriVide Original D65 Tube light
The VeriVide D65 Artificial Daylight Tube is suitable for applications where standardized daylight illumination is required for visual inspection and colour assessment.
Textile Industry
The textile and garment industry is one of the major applications for D65 artificial daylight.
Textile manufacturers, dyeing factories, garment factories, buying houses and quality-control laboratories need to compare fabric samples, dyed yarns, garments and colour standards under controlled lighting.
Typical applications include:
- Fabric shade matching
- Garment colour inspection
- Yarn colour comparison
- Dyed fabric inspection
- Colour approval
- Lab dip assessment
- Bulk production shade checking
- Colour standard comparison
- Final garment inspection
- Buyer sample approval
Using standardized lighting helps different departments and organizations evaluate the same colour under similar viewing conditions.
Colour Matching
Colour matching requires more than simply checking whether two samples look similar.
A sample may appear acceptable under one light source but show a noticeable difference under another light source. This is particularly important in textile, garment and manufacturing applications.
VeriVide Original D65 Tube light provides a standardized daylight reference for visual assessment.
For example, a laboratory may compare:
Approved Colour Standard → Lab Dip → Bulk Fabric
All three samples can be evaluated under the same D65 lighting condition.
This provides a more controlled environment for colour decisions.
Metamerism Assessment
Metamerism occurs when two colours appear to match under one lighting condition but appear different under another.
This can create serious problems in textile and product manufacturing.
For example:
- Fabric A may match the approved standard under one light.
- Under daylight, Fabric A may appear different.
- Under store lighting, the difference may become even more noticeable.
VeriVide Original D65 Tube light recommends standardized viewing environments because changing illumination can reveal colour differences that may not be visible under another light source.
VeriVide Original D65 Tube light light source can therefore form an important part of a professional colour assessment system.
Use in VeriVide Colour Assessment Cabinets
VeriVide colour assessment cabinets can be configured with standardized light sources including D65 and D50, along with other illuminants depending on the application.
The D65 tube is particularly useful where daylight-standard colour assessment is required.
A typical colour assessment cabinet may contain multiple light sources to allow the operator to check colour behaviour under different lighting conditions.
This can help identify:
- Colour inconsistency
- Metamerism
- Shade variation
- Fluorescence-related appearance
- Differences between product and colour standard
Use in Textile Testing Laboratories
Textile testing laboratories require controlled and repeatable environmental conditions for visual assessments.
VeriVide Original D65 Tube light can be used as part of an appropriate viewing cabinet or visual inspection system for:
- Colour fastness assessment
- Shade evaluation
- Fabric colour grading
- Garment inspection
- Pilling assessment
- Appearance assessment
- Colour matching
- Standard comparison
VeriVide Original D65 Tube light own textile testing equipment uses CIE D65 artificial daylight for standardized visual assessment applications. For example, its Pilling Assessment Viewer uses VeriVide CIE D65 Artificial Daylight for assessment under relevant EN ISO 12945 methods.
Colour Fastness Assessment
Visual evaluation is also important in textile colour fastness testing.
A controlled D65 light source can provide standardized viewing conditions when comparing test specimens with reference standards.
VeriVide's Colour Fastness Cabinet, for example, uses D65 Artificial Daylight at 6500K as one of its standardized light sources, together with UV black light for relevant assessment applications.
Benefits for Garment Manufacturers
For garment manufacturers, colour consistency is essential from sampling through bulk production.
The VeriVide Original D65 Tube light can help establish a controlled visual environment for:
Sampling
Compare the original colour standard with lab dips and development samples.
Production
Check whether bulk production remains within the approved colour range.
Quality Control
Evaluate finished garments before shipment.
Buyer Inspection
Provide a standardized environment for colour approval.
Final Inspection
Reduce the possibility of colour disputes caused by inconsistent lighting.
Benefits for Textile Dyeing Factories
In dyeing factories, colour decisions are often made at several stages.
These may include:
- Recipe development
- Lab dip preparation
- Lab dip approval
- Bulk dyeing
- Shade checking
- Finishing
- Final inspection
- Shipment inspection
Using a standardized VeriVide Original D65 Tube light source can help maintain consistent visual conditions across these stages.
This is especially useful when several people are involved in colour evaluation.
Standards and Compliance
The VeriVide Original D65 Tube light is specified by VeriVide for use as a D65 artificial daylight source.
According to VeriVide's published lamp information, the D65 lamp has a 6500K correlated colour temperature, is within the tolerances prescribed in BS 950 Part 1, and has high conformance to relevant CIE specifications for accurate colour matching. VeriVide's current documentation also references ISO/CIE 23603 / CIE S 012/E for D65 applications.
Depending on the particular testing method, viewing cabinet and industry application, additional standards may apply. Users should always verify the exact lighting requirements specified by their applicable test method, buyer or customer.
Why Standardized Lighting Matters
Natural daylight is not constant.
It can change due to:
- Time of day
- Weather
- Season
- Geographic location
- Atmospheric conditions
- Window orientation
- Surrounding environment
Because of these factors, a colour sample may look different at different times or locations.
VeriVide notes that these natural-light variations can cause colour consistency problems throughout a supply chain. Standardized artificial light provides a controlled alternative.
For international textile and garment supply chains, this is especially important because a buyer, manufacturer and supplier may be located in different countries.
VeriVide D65 vs Ordinary Daylight
| Feature | VeriVide D65 | Ordinary Natural Daylight |
|---|---|---|
| Standardized | Yes | No |
| Colour Temperature | 6500K | Variable |
| Controlled Environment | Yes | No |
| Colour Assessment | Professional | Variable |
| Repeatability | High | Low |
| Weather Dependent | No | Yes |
| Time-of-Day Dependent | No | Yes |
| Suitable for Standardized Colour Evaluation | Yes | Not recommended as sole reference |
The purpose of VeriVide D65 is therefore to provide a more consistent and controlled lighting condition than relying on natural daylight alone.
VeriVide Original D65 Tube Replacement
For existing VeriVide viewing cabinets and compatible systems, correct lamp replacement is important.
VeriVide recommends replacing lamps after their specified service life because the spectral output of lamps can change with usage. The manufacturer notes a 2000-hour life-cycle recommendation for its lamps and recommends replacement after 2000 hours or one year of use to maintain reliable colour assessment conditions.
When replacing a lamp, users should verify:
- Correct VeriVide D65 specification
- Correct tube length
- Correct wattage
- Correct tube type
- Compatibility with the existing equipment
- Applicable voltage and ballast requirements
How to Select the Correct D65 Tube
Before ordering a replacement VeriVide D65 tube, check the existing lamp.
Step 1 – Check the Length
Measure the existing tube.
Available VeriVide D65 lengths include:
- 600 mm
- 1200 mm
- 1500 mm
Step 2 – Check Wattage
The corresponding official specifications are:
- 600 mm – 18W
- 1200 mm – 36W
- 1500 mm – 58W
Step 3 – Check Tube Type
The listed D65 versions are T8.
Step 4 – Check Equipment Compatibility
If the lamp is being installed into a VeriVide viewing cabinet or colour assessment equipment, confirm the equipment model before ordering.
Step 5 – Confirm Original Product Requirement
For professional colour assessment, use the correct standardized lamp rather than an ordinary commercial daylight tube.
Suitable Industries
The VeriVide Original D65 Tube Light can be relevant to many industries, including:
Textile & Garments
Fabric, yarn, garment and shade evaluation.
Dyeing & Finishing
Lab dip and bulk shade comparison.
Printing
Visual colour checking of printed materials.
Packaging
Colour consistency of packaging materials.
Plastics
Colour and appearance inspection.
Paint & Coating
Visual colour comparison.
Automotive
Component colour and appearance assessment.
Furniture
Fabric, leather, plastic and surface colour evaluation.
Graphic Arts
Visual inspection under controlled lighting where the relevant D65 specification is applicable.
Key Features at a Glance
VeriVide Original D65 Tube light offers:
- Original VeriVide D65 light source
- 6500K correlated colour temperature
- CRI 98
- T8 tube format
- Multiple length options
- Standardized artificial daylight
- Professional colour assessment
- Consistent visual inspection conditions
- Suitable for textile and garment industries
- Suitable for colour matching
- Useful for metamerism assessment
- Suitable for compatible VeriVide equipment
- Professional replacement lamp solution
Frequently Asked Questions
What is a VeriVide D65 Tube Light?
VeriVide D65 is a standardized artificial daylight lamp designed to provide controlled D65 illumination for professional visual colour assessment.
What is the colour temperature of VeriVide D65?
The VeriVide D65 Artificial Daylight Tube has a correlated colour temperature of 6500K.
What is the CRI of VeriVide Original D65 Tube light ?
The official VeriVide specification lists the D65 lamp with CRI 98.
What lengths are available?
The official specification lists 600 mm, 1200 mm and 1500 mm versions.
What are the wattages?
The listed versions are 18W, 36W and 58W, corresponding respectively to 600 mm, 1200 mm and 1500 mm lengths.
Is VeriVide Original D65 Tube light suitable for textile colour matching?
Yes. D65 standardized daylight is widely used in controlled visual colour assessment, including textile and garment applications. VeriVide specifically describes D65 as being specified for applications where colour consistency and quality need to be maintained.
Why should I use Original VeriVide D65 instead of an ordinary 6500K tube?
A tube being labelled “6500K” does not by itself make it a standardized VeriVide D65 colour-assessment lamp. Professional colour assessment depends on the characteristics of the light source, not only its nominal colour temperature. VeriVide's D65 lamp is designed and specified as an artificial daylight source for standardized colour assessment.
When should the D65 lamp be replaced?
VeriVide recommends replacement after approximately 2000 hours or one year of use to maintain reliable assessment conditions.
Can this lamp be used in any T8 fixture?
Not necessarily. Compatibility with the fixture, ballast, electrical requirements and intended application should be checked before installation.
Product Applications
VeriVide D65 Artificial Daylight Tube Light is suitable for:
- Textile Testing Laboratory
- Garment Factory
- Dyeing Factory
- Fabric Inspection
- Colour Matching Laboratory
- Quality Control Laboratory
- Buying House
- Apparel Industry
- Printing Industry
- Packaging Industry
- Plastic Industry
- Paint Industry
- Product Inspection
- Colour Assessment Cabinet
- Viewing Cabinet
- Visual Inspection System
Why Buy VeriVide D65 from MAAM TEX?
MAAM TEX supplies textile testing instruments, laboratory equipment, colour assessment products and related consumables for textile and garment industries.
For customers requiring VeriVide Original D65 Artificial Daylight Tube Light, we can provide the appropriate specification based on your existing equipment, required tube length and application.
Before placing an order, please provide:
- Required quantity
- Tube length – 600 / 1200 / 1500 mm
- Existing machine/cabinet model, if applicable
- Required wattage
- Photo of the existing tube, if available
This information helps ensure that the correct replacement lamp is supplied.
Ordering Information
Product:
VeriVide Original D65 Tube Light – Artificial Daylight
Available Options:
600D65
600 mm / 18W / T8 / 6500K / CRI 98
1200D65
1200 mm / 36W / T8 / 6500K / CRI 98
1500D65
1500 mm / 58W / T8 / 6500K / CRI 98
current stock Available
Conclusion
The VeriVide Original D65 Tube Light – Artificial Daylight is a professional standardized daylight source for controlled visual colour assessment. With 6500K colour temperature and CRI 98, it is designed for applications where colour consistency, repeatability and accurate visual evaluation are important.
For textile and garment manufacturers, dyeing factories, testing laboratories, buying houses and quality-control departments, a standardized D65 lighting environment can help create more consistent colour evaluation conditions and reduce problems associated with variable natural daylight.
For compatible VeriVide equipment and professional colour assessment applications, selecting the correct Original VeriVide D65 lamp is important for maintaining the intended lighting conditions of the system.
Color Matching Cabinet-Light Box
Color Matching Cabinet-Light Box
Color Matching Cabinet-Light Box
fabric moisture permeability tester
Fabric Moisture Permeability Tester
Fabric Moisture Permeability Tester
Fabric Moisture Permeability Tester
- Upright Cup Method: The fabric covers a cup containing water, and the assembly is placed upright in a controlled environment. After a set duration, the weight loss is measured to determine the WVTR.
- Inverted Cup Method: The fabric is sealed over a cup, which is then inverted and exposed to a controlled environment. The amount of water vapor absorbed by the fabric is measured over time.
- Sweating Hot Plate Test: Simulates human perspiration by measuring the energy required to maintain a constant temperature on a heated plate covered with the fabric, providing insights into the fabric's breathability.
- Multi-Cup Design - Typically includes 6 or more test cups for simultaneous testing of multiple samples.
- Rotating Turntable - Ensures uniform air exposure and consistent vapor transmission across all samples.
- Precision Weighing System- Accurate measurement of weight loss to calculate water vapor transmission rate (WVTR).
- Temperature & Humidity Control - Maintains stable environmental conditions (e.g., 23°C, 50% RH) for reliable results.
- Digital Display or Software Interface - Displays real-time data and test status; advanced models offer data logging and export.
- Compliance with Standards - Supports ASTM E96, ISO 15496, BS 7209, JIS L1099 testing methods.
- Sealed Test Chambers- Prevents external air interference, improving accuracy.
- Corrosion-Resistant Construction - Durable materials suitable for long-term use in lab environments.
- Easy Sample Mounting - Quick and secure fabric placement on test cups with sealing rings.
- Low Maintenance Design- Simplified components for easy cleaning and upkeep.
- Prepare the Test Solution - Fill each test cup with a set amount of water (e.g., 50 ml), or a desiccant if using inverted method.
- Mount the Fabric - Cut the fabric into circular pieces matching the cup size.
- Weigh the Cups - Record the initial weight of each cup with the fabric mounted.
- Place on Turntable - Position all cups on the rotating tray inside the controlled chamber.
- Set Conditions - Close the chamber and maintain temperature (e.g., 23°C) and relative humidity (e.g., 50%) as per test standard.
- Start the Test - Begin rotation (usually ~2 RPM) and let it run for the specified time (often 24 hours).
- Weigh the Cups Again- After the test duration, reweigh the cups to determine weight loss due to moisture vapor passing through the fabric. Calculate WVTR - Use the formula: WVTR = (Weight Loss in grams × 24) / (Test Area in m² × Time in hours) Expressed in g/m²/24h.Clean and Store - Clean cups and components for future use.
 Scope of application
It is used to determine the moisture permeability of various fabrics
(including moisture permeable coated fabrics)
and nonwovens such as batting cotton and space cotton.
[Related standards] GB/T12704 ASTM E90 JIS L1099A BS 7209 JIS L1099B (custom) etc.
Instrument characteristics
1. Integrated structure of baking oven and constant temperature and humidity box.
2. Microcomputer control, color touch screen Chinese menu operation.
3. Circulating air velocity 0.2-3m/s digital setting.
4. Imported high-precision temperature and humidity sensor, imported motor drive, ceramic
heating tube heating.
Technical parameters
1.Work mode: Microcomputer control, color touch screen Chinese menu operation, test environment monitoring.
2. Sample box control temperature:15 ~ 40 C, accuracy 0.1 + C, resolution 0.01 C
3. Heat dissipation mode:Air cooling
4. Sample box control humidity:30 ~ 95%, precision + 2%, resolution 0.01%
5. Test chamber humidification:≥300ml/h
6. Accompany oven control temperature: Room temperature to 200 c
7. Test time:1min~999h59min
8. The rate of circulating steam flow:0. 2-3m/s digital setting resolution 0.01m/s
9. Moisture permeability area:2827㎜2(∮60㎜GB)
Optional 3848, 2 (70 70 ASTM)
10. The number of moisture permeable cups.6 (GB) can be replaced by 6 (US standard).
11. Internal dimensions of drying oven:490×400×215mm
12. Power supply:Ac220V 50Hz 6kw
13. Size:930×820×1700mm
14. Weight:350kg

Bursting strength tester
Bursting strength tester

true burst
- Available with automatic test strip feeder Measurements are simple to make with the Mullen type Bursting Strength Tester. Fast automatic measurements Measurement starts automatically once a test piece has been placed in the measuring gap. The clamping foot descends, and a bursting strength measurement is made.
- Bursting pressure can reach up to 1.2MPa 5. The maximum burst and expansion degree can reach 70mm. 6. Strengthen the lighting system on the test surface. 7. The main aerodynamic force helps to clamp the sample system. 8. A variety of test areas are available, and the switching is easy.
- A variety of unit conversions between Chinese and English. 10. Reliable anti-pinch safety protection design. [Technical parameter]: 1. Test range: (0~1)Mpa (the range above 1Mpa needs to be customized) 2. The minimum graduation value: 0.0001Mpa 3. Pressurization mode: direct pressurization, timing pressurization, and expansion degree pressurization.

Gray scale
Gray Scale
Gray Scale
- Gray Scale for Color Change - Compares the original and tested sample to measure color fading or alteration.
- Gray Scale for Staining - Compares a white adjacent fabric (before and after testing) to assess color transfer or staining.
- Standardized Evaluation - Provides a consistent and objective way to assess color change or staining.
- Simple and Quick to Use - Enables rapid visual comparison during fabric testing.
- Widely Accepted - Complies with international standards (ISO, AATCC) for color fastness grading.
- Cost-Effective Tool - Inexpensive yet essential for reliable quality control in textiles.
- Enhances Quality Assurance - Helps detect dyeing or printing issues before bulk production.
- Supports Multiple Tests - Used for evaluating wash fastness, rubbing fastness, perspiration, light exposure, and more.
- Portable and Durable - Easy to carry and long-lasting with proper care.
- Dual Type Availability - Comes in two types: for Color Change and for Staining.
- 5-Point Grading System - Grades from 1 (poor) to 5 (excellent), with half-step intervals like 4–5, 3–4.
- Standardized Grey Chips - Includes contrasting grey color pairs to match fabric changes accurately.
- Compact Design - Small, portable card or booklet format for easy lab and field use.
- Durable Material - Made from stable, fade-resistant plastic or cardboard for long-term use.
- Compliance with Standards - Follows ISO 105-A02 (Color Change) and ISO 105-A03 (Staining) norms.
- Easy Visual Comparison - Designed for quick side-by-side assessment of fabric before and after testing.
- Place the Samples - Lay the untested (original) and tested fabric side by side (for color change)
- Match Against Gray Scale Chips - Visually compare the difference between the samples and find the closest matching gray pair on the scale.
- Assign a Grade
- Record the Result - Note the grade in your test report as per the test method (e.g., ISO 105).
- Store Properly - Keep the gray scale away from light and moisture to avoid fading.
- Features :
- Dual Type Availability - Comes in two types: for Color Change and for Staining.
- 5-Point Grading System - Grades from 1 (poor) to 5 (excellent), with half-step intervals like 4–5, 3–4.
- Standardized Grey Chips - Includes contrasting grey color pairs to match fabric changes accurately.
- Compact Design - Small, portable card or booklet format for easy lab and field use.
- Gray Scale for Color Change - Used to evaluate the degree of color fading or change in a fabric after testing (e.g., washing, light exposure). - Assesses how much the original color has altered.
- Gray Scale for Staining - Used to assess the degree of color transfer from a dyed fabric to an adjacent white fabric during testing (e.g., rubbing, washing).
Gray Scale
Digital Temperature Humidity Meter
Digital Temperature Humidity Meter
Digital Temperature Humidity Meter
Fabric drape tester
Fabric Drape Tester
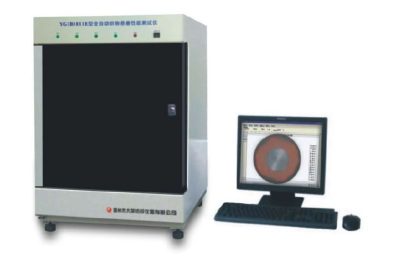
Fabric Drape Tester
- Quantifies Fabric Flow - Measures drape behavior accurately, crucial for garments and furnishings.
- Supports Design Decisions - Helps designers select fabrics that match the intended look and movement of a product.
- Improves Garment Fit and Comfort - Ensures fabrics behave naturally on the body, enhancing wear ability.
- Enhances Product Aesthetics - Prevents stiff or limp fabric choices in fashion, interior, or technical textiles.
- Standardized Evaluation - Enables comparison across fabrics using drape coefficient, based on standards (e.g., BS 5058).
- Supports R&D - Useful in developing new fabrics or finishes to improve drape quality.
- Non-Destructive Testing - Tests fabric without damaging it, allowing for further analysis.
- Boosts Quality Control - Identifies batch inconsistencies or performance issues early in production.
- Rotating Support Disc - Holds the fabric sample over a smaller disc to create natural drape.
- Standard Sample Size Support - Designed for circular fabric samples, usually 30 cm in diameter.
- Light Projection System - Projects the draped fabric’s shadow onto a screen or recording surface.
- Drape Coefficient Calculation - Measures the shadow area to compute the drape coefficient (percentage of unsupported area covered by the shadow).
- Digital or Manual Options - Available in models with digital image processing or manual plan meter tracing.
- Stable Base and Structure - Ensures consistent and vibration-free testing conditions.
- Sample Templates Provided - For cutting precise, standard-sized fabric specimens.
- User-Friendly Interface - Simple controls for rotation and light alignment.
- Compact and Lab-Ready Design - Fits easily on lab benches and in testing environments.
- Compliance with Testing Standards - Supports BS 5058 and other relevant drape measurement methods.
- Prepare the Fabric Sample - Cut a circular fabric sample, typically 30 cm in diameter, using the provided template.
- Place the Fabric - Center the fabric sample over the smaller support disc (usually 18 cm diameter) on the tester.
- Turn on the Light Source - Illuminate the fabric from above so it casts a shadow onto the recording surface or paper below.
- Capture the Shadow Outline - Trace the shadow manually on paper or capture it digitally, depending on the model.
- Measure the Shadow Area - Use a plan meter (manual) or software (digital) to determine the shadow’s area.
- Calculate Drape Coefficient (DC) - Use the formula:
- Record the Result - Log the drape coefficient to evaluate how stiff or flexible the fabric is.
- Repeat for Accuracy - Test multiple samples and average the results for consistency.
 It is used for testing dynamic and static drape properties
(drape coefficient, shape change rate, surface ripple and drape uniformity, etc.)
of various fabrics.
Related standards GB/T23329 FZ/01045 BS5058 etc.
Instrument characteristics
1. CCD imaging, dynamic and static image processing.
2. A variety of charts and data statistics, analysis, storage, output
3. No need to replace background color, can test all kinds of color samples.
4. Work mode:Microcomputer control, CCD imaging, automatic processing of images and data automatically.
Technical parameters
1. Communication interface: RS232, USB
2. Image sensor: CCD sensor.
3. Static (dynamic) state draping coefficient: 0 ~ 100% + 2
4. Drapability uniformity: 0 ~ 100% + 2
5. The rate of morphological change is 0 to 100% + 2.
6. Surface waviness error: + 1

